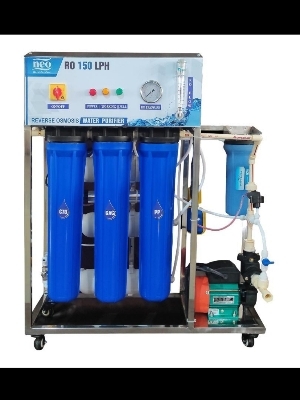
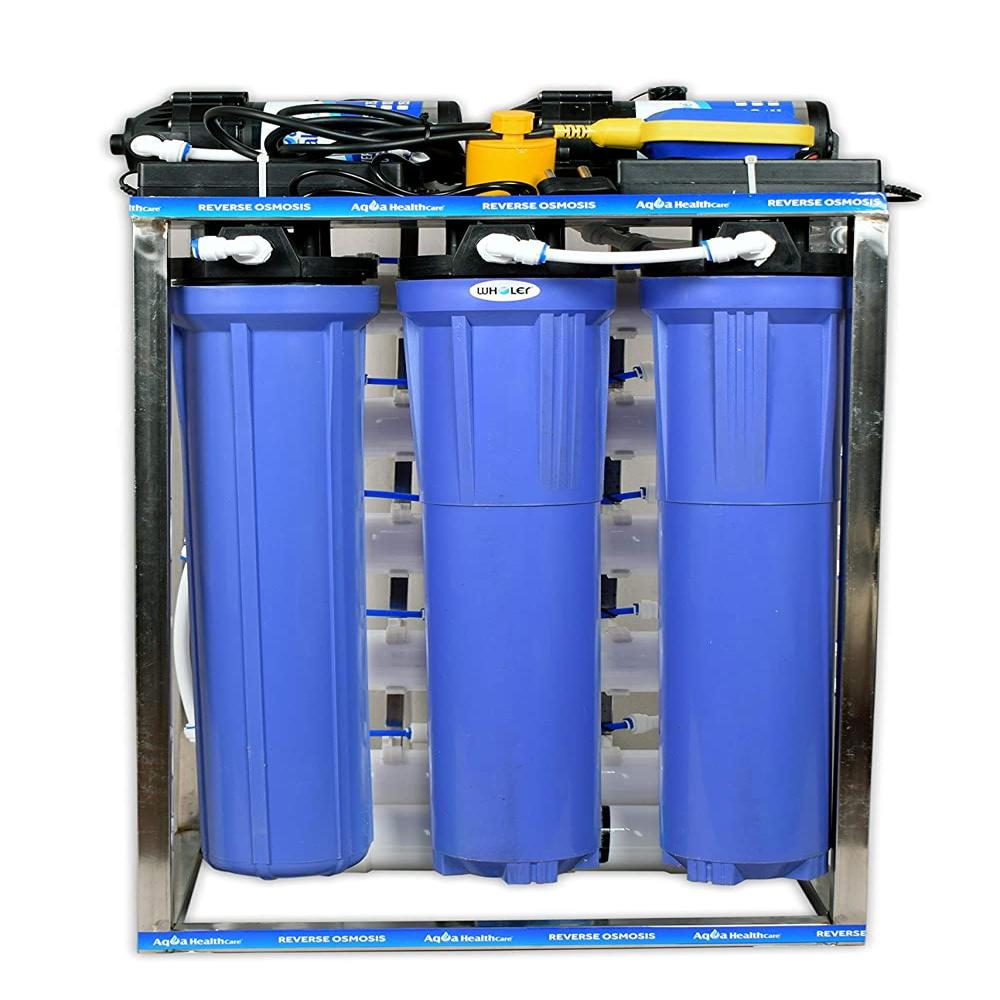
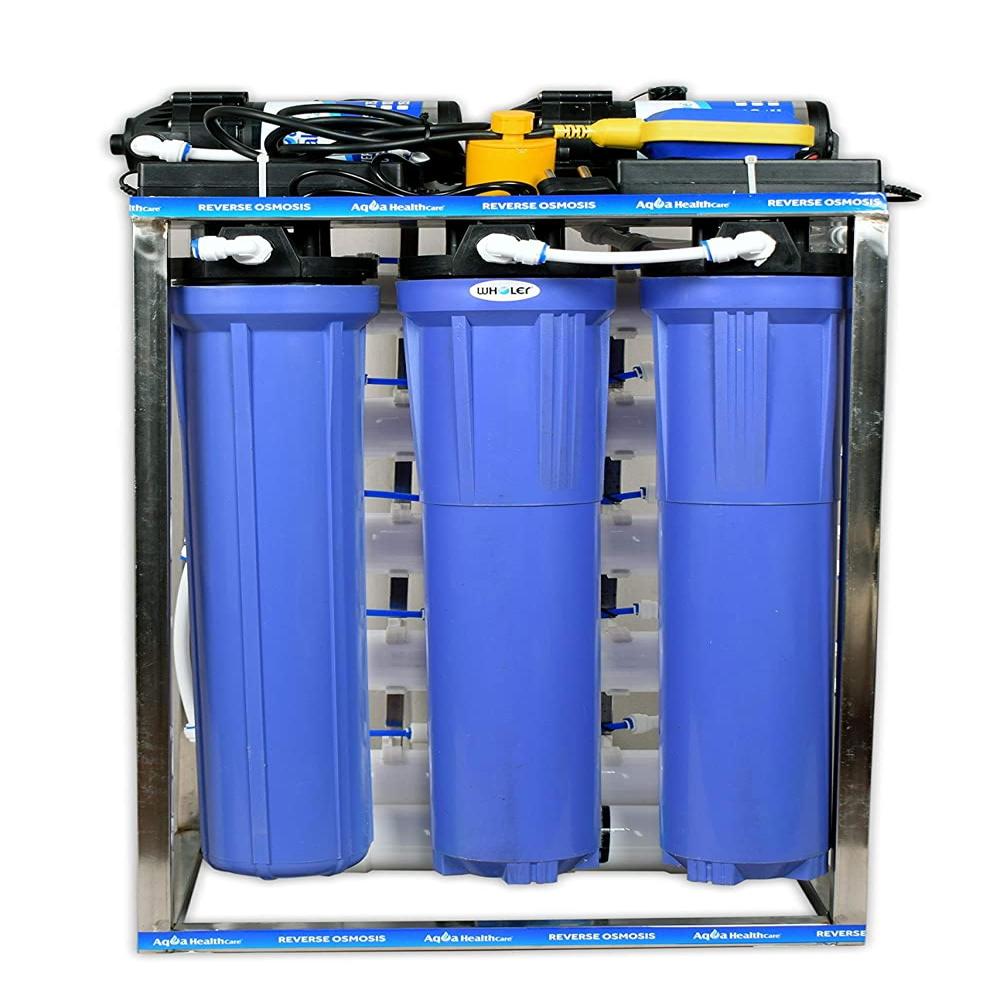
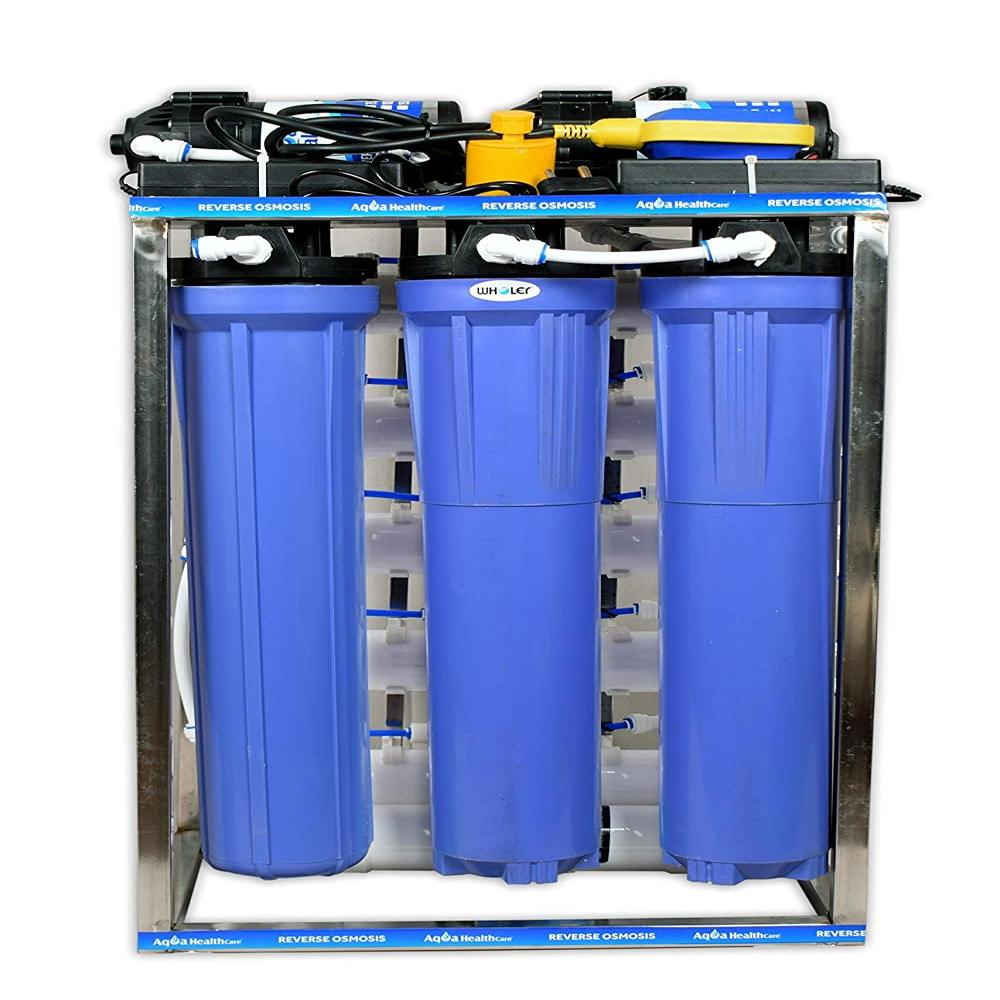
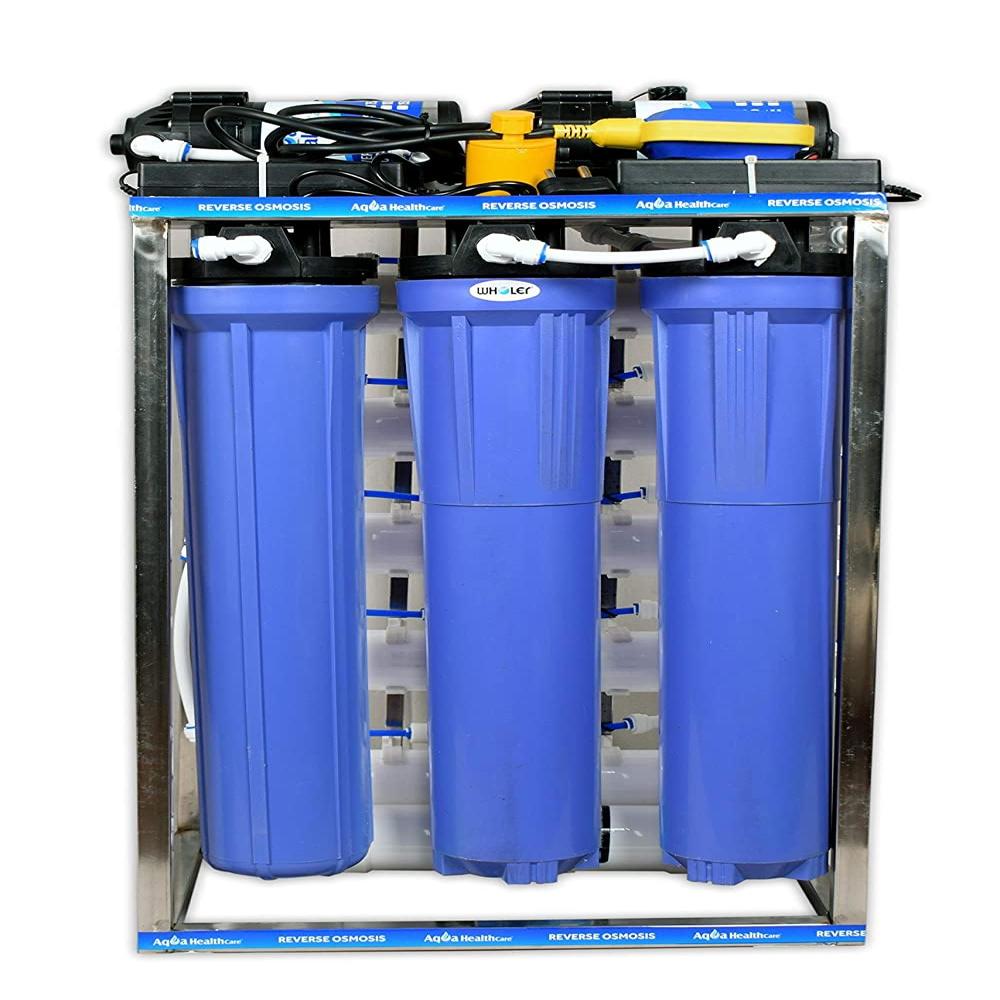
About Fully Automatic ro plants 150 lph
Pre-Treatment Sand filter and activated carbon filter, as required Structure SS / MS, as required Power Supply 220V AC, subject to configuration Application Offices, hotels, hospitals, schools and factories Key Features Automatic operation and water-level control Efficient dissolved-solids reduction Compact and easy-to-maintain design Optional UV sterilization and TDS controller Customizable according to raw-water quality Suitable for: Commercial drinking-water purification and small industrial applications. For a suitable plant configuration, the feed-water TDS and required daily water consumption should be confirmed first.
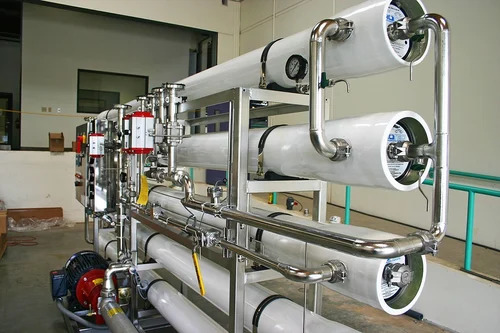
Advanced Technology for Reliable Water PurificationUtilizing the latest reverse osmosis technology, this plant guarantees high purity water. Its combination of pre-filtration and multistage RO ensures contaminants are thoroughly removed, delivering consistent water quality for diverse commercial and institutional applications.
Efficient and User-Friendly OperationThe fully automatic system minimizes the need for manual intervention, while its energy-efficient design keeps operational costs low. Built to handle varying raw water qualities, the plant's robust high-pressure pump and automatic controls ensure reliable performance and easy maintenance.
Versatile Applications and Durable BuildCrafted from high-grade FRP, MS, or SS materials, the RO plant is engineered for longevity. Its low noise level and compact design make it suitable for various environments, from schools and hospitals to hotels and laboratories, offering adaptability and dependable service.
FAQ's of Fully Automatic ro plants 150 lph:
Q: How does the fully automatic RO plant ensure high purity water output?
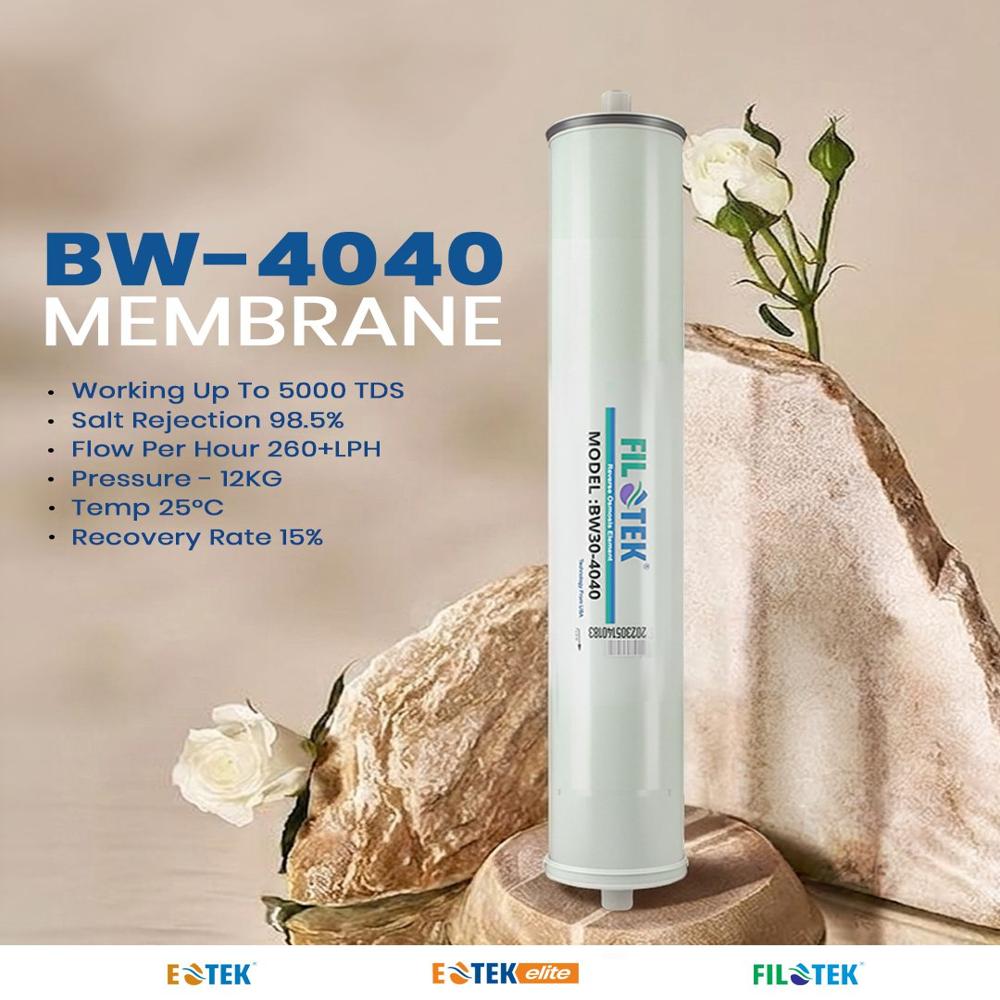
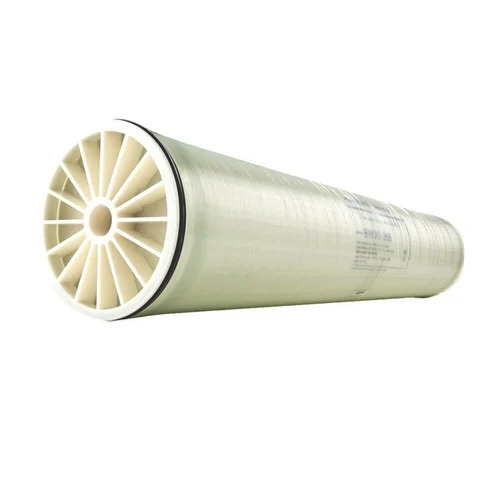
A: The plant uses a multi-stage filtration process, including sand, carbon, and micron filters, followed by reverse osmosis membranes. Coupled with automatic operation, this sequential purification efficiently removes dissolved salts, impurities, and contaminants, delivering water with typical conductivity below 50-100 S/cm.
Q: What are the recommended usage scenarios for this 150 LPH RO plant?
A: This RO plant is ideal for commercial, industrial, hospital, school, hotel, restaurant, and laboratory settings where a continuous supply of high-purity water is required. Its durable construction allows it to handle varied water sources and demanding operational environments.
Q: When should routine maintenance be performed on this RO plant?
A: Although the system is designed for low maintenance, routine checks are recommended monthly. This includes monitoring pre-filters, checking membrane integrity, and assessing pump performance to ensure consistent output and extend component life.
Q: Where can the 150 LPH RO plant be installed?
A: The plant's compact structure and low noise levels make it suitable for indoor installation in commercial or institutional premises, including basements, equipment rooms, or dedicated utility spaces. It should be placed near a steady electric supply and accessible water source.
Q: What is the water recovery process in this RO plant?
A: The RO plant recycles a portion of the feed water, typically achieving a recovery rate of 40-60%, depending on raw water quality. The system reuses part of the reject water, thereby conserving resources and reducing total water wastage.
Q: How does the automatic operation benefit the user?
A: Automatic operation streamlines the purification process, requiring minimal user intervention. It monitors and adjusts pressures, flows, and cleaning cycles, which reduces downtime, minimizes the risk of operator error, and ensures consistent water quality output.
Q: What are the energy and power requirements for this model?
A: The plant operates on a 220-240V AC supply at 50Hz, with power consumption depending on feed pressure but typically in the range of 8-15 kW. The high-pressure multistage pump and energy-efficient design help reduce overall electricity costs.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
